Case Studies

Real industrial applications of spectroscopy intelligence — from field trials to live operational deployments.

Case Study Maturity Levels

Feasibility — Early proof of concept Pilot — Small-scale operational trial Validated — Correlated against reference methods Operational — Live field or process deployment

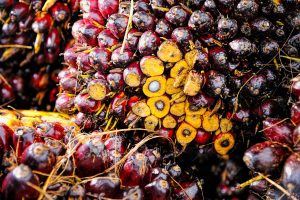
Case Studies Real industrial applications of spectroscopy intelligence — from field trials to live operational deployments. Palm Oil: Fresh Fruit Bunch (FFB)

Sustainability Benefits of NIR Spectroscopy

IR Spectroscopy: The Smart Way Towards Farming Sustainability

⚡ Quick Assessment

Quick and accurate assessment of material quality at various control points across the supply chain — from farm gate to factory floor.

📈 Data-Driven Decisions

Provides immediate, valuable process data — empowering data-driven decisions rather than relying on delayed laboratory results.

🌱 Reduced Carbon Footprint

Significantly reduces carbon footprint by optimising resource usage and eliminating reagent waste from destructive testing methods.

🏭 Increased Productivity

Maximises efficiency of energy utilisation, resulting in higher product yield and reduced operational overhead per tonne.

♻️ Green Technology

NIR reduces hazardous chemical waste during quality testing — non-destructive, reagent-free and environmentally clean by design.

🫙 Enhanced Oil Extraction

Quick and accurate oil content prediction leads to greater Oil Extraction Rate (OER) and reduced palm oil losses across the milling process.

Pharmaceutical & PAT Case Studies

The following case studies are in preparation. Contact us to discuss a similar application in your facility.

In Development Pharma / Chemical

Raw Material ID Through Opaque Packaging

SORS/NIR screening of incoming pharmaceutical raw materials through containers — eliminating 48-hour lab bottlenecks for incoming component release.

In Development Pharma

NIR Moisture Prediction vs Karl Fischer Titration

Non-destructive moisture prediction replacing slow, destructive KF titration — with NIR models validated to pharmaceutical regulatory standards.

Feasibility Pharma Manufacturing

Real-Time Powder Blend Uniformity Monitoring

In-line NIR monitoring during pharmaceutical powder blending — detecting blend endpoints and preventing batch failure from blend non-uniformity.

Working on a Similar Application?

Tell us your industry, sample type and target parameter — we’ll assess whether spectroscopy can solve it.